 EN
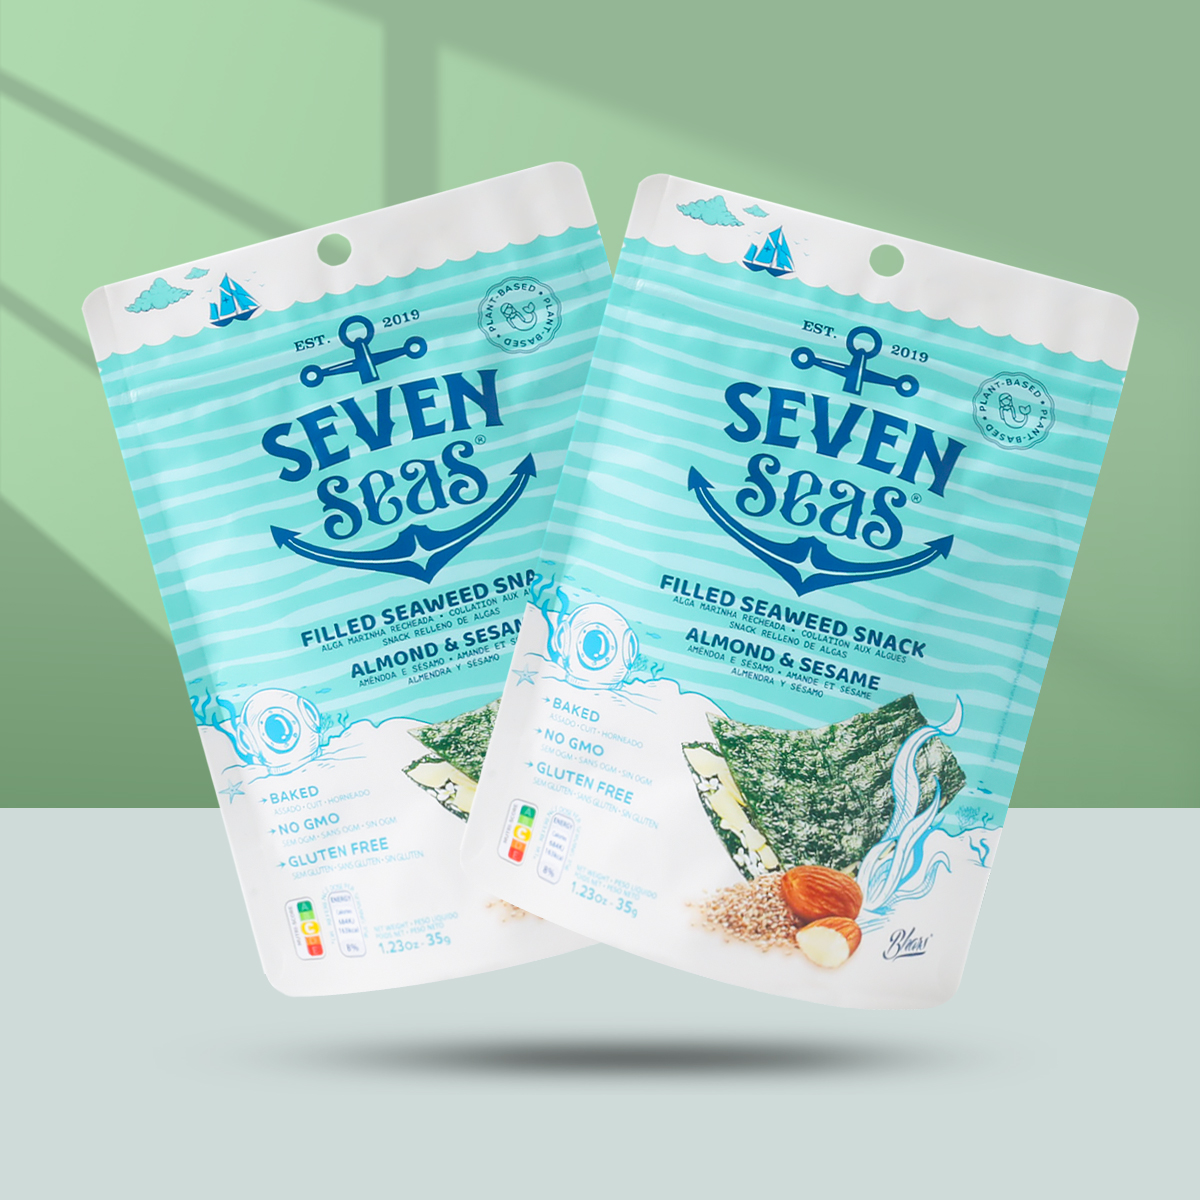
Industrial and chemical manufacturers face persistent packaging challenges that directly impact product integrity, operational efficiency, and market competitiveness. Heavy-duty stand up pouch solutions have emerged as a transformative packaging option that addresses these challenges with robust design, superior barrier protection, and flexible scalability. Unlike traditional rigid containers or lightweight films, a stand up pouch combines structural stability with protective properties, making it ideal for demanding applications where product safety and shelf presence are non-negotiable. This article explores how stand up pouch technology delivers measurable value across industrial and chemical product categories, examining the engineering principles, material specifications, and practical deployment strategies that make this packaging format essential for modern manufacturing operations.
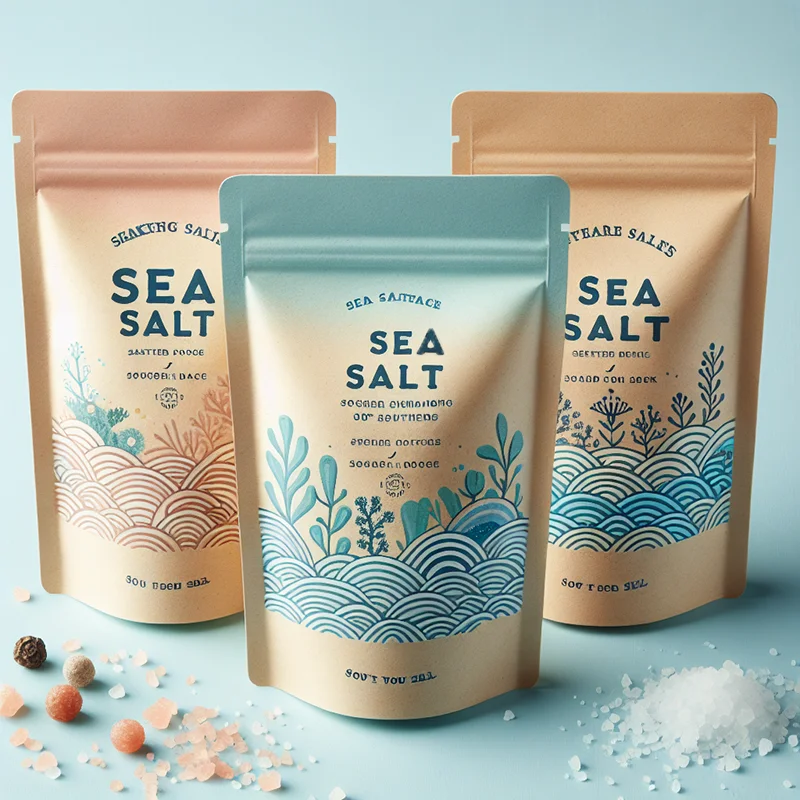
The industrial packaging landscape demands solutions that exceed basic containment functionality. A stand up pouch provides multiple layers of protection against moisture, oxygen, light, and physical damage while maintaining cost efficiency at scale. For chemical manufacturers, pharmaceutical distributors, and specialty product suppliers, selecting the right stand up pouch configuration directly influences product shelf life, regulatory compliance, and brand perception. Understanding the structural, material, and functional advantages of stand up pouch packaging enables purchasing managers and operations teams to make informed decisions that optimize both product protection and supply chain performance.
Superior Barrier Protection and Material Engineering
Multi-Layer Film Construction for Chemical Resilience
Heavy-duty stand up pouch designs employ multi-layer film technology that creates comprehensive barriers against environmental threats. Each layer serves a specific protective function: outer layers provide puncture and tear resistance, middle layers block moisture and oxygen transmission, and inner layers ensure chemical compatibility and seal integrity. A stand up pouch engineered for industrial chemicals incorporates high-performance films such as polyester, polyethylene, and aluminum foil laminates that resist corrosive substances, prevent vapor transmission, and maintain structural rigidity under pressure. This layered approach ensures that a stand up pouch protects sensitive formulations, powders, liquids, and granular materials across diverse industrial applications without compromising seal reliability or product quality.
Aluminum Foil and Metallized Barrier Solutions
For maximum protection, industrial stand up pouch options incorporate aluminum foil layers that provide absolute barrier to light, moisture, and gases. An aluminum-enhanced stand up pouch extends product shelf life significantly, particularly for photosensitive chemicals, oxidation-prone compounds, and hygroscopic powders that degrade rapidly when exposed to environmental factors. The stand up pouch with metallized films offers an alternative for applications requiring cost optimization while maintaining superior barrier performance. These material combinations ensure that a stand up pouch meets stringent industry standards, regulatory requirements, and customer expectations for product integrity throughout the entire supply chain lifecycle.
Structural Stability and Shelf-Ready Performance
Gusseted Construction and Load-Bearing Capacity
The distinctive advantage of a stand up pouch lies in its engineered gusseted base and reinforced sidewalls that enable independent standing on retail shelves, warehouse pallets, and distribution displays. A properly designed stand up pouch maintains vertical orientation under substantial weight, protecting contents from crushing damage and enabling efficient stacking in logistics networks. The gusset design of a stand up pouch distributes pressure evenly across the base, preventing deformation and seal separation that compromise product integrity. Industrial manufacturers benefit from stand up pouch configurations that accommodate larger volumes, heavier products, and aggressive handling conditions while preserving structural integrity from manufacturing through end-use consumption.
Seal Integrity and Contamination Prevention
Advanced seal technologies integrated into heavy-duty stand up pouch designs create hermetic closures that prevent contamination, moisture ingress, and product loss. A stand up pouch with zipper mechanisms, press-to-close seals, or induction-heat seals ensures that products remain protected after opening or during storage intervals in demanding industrial environments. The seal performance of a stand up pouch directly correlates with product shelf life, regulatory compliance for chemical products, and customer satisfaction across industrial distribution channels. Superior sealing technology distinguishes a high-performance stand up pouch from basic alternatives, ensuring that contents remain uncompromised throughout extended storage, temperature fluctuations, and rough handling scenarios common in industrial operations.
Cost Efficiency and Scalable Production
Reduced Material Consumption and Shipping Advantages
A stand up pouch achieves superior resource efficiency compared to rigid containers, glass packaging, or traditional plastic drums. The lightweight nature of a stand up pouch reduces transportation costs, warehouse storage requirements, and packaging material waste, directly improving operational profitability across supply chains. Industrial manufacturers achieve significant cost reductions by transitioning to stand up pouch solutions that consolidate multiple protective functions into a single, optimized package. The scalability of stand up pouch production allows manufacturers to adjust order quantities, customize specifications, and respond rapidly to market demand without investing in expensive equipment changes or extended lead times.
Customization and Brand Differentiation
Modern stand up pouch manufacturing capabilities enable extensive customization including custom printing, color coding, material selection, and size optimization tailored to specific product requirements. A branded stand up pouch enhances product visibility, communicates technical specifications, and reinforces brand identity in competitive industrial markets. The flexibility of stand up pouch design allows manufacturers to incorporate safety warnings, regulatory compliance information, and usage instructions directly on packaging, improving product safety and customer communication. Investment in premium stand up pouch customization delivers measurable returns through enhanced product recognition, reduced customer confusion, and improved market positioning for specialized industrial and chemical products.
FAQ
What industries benefit most from stand up pouch packaging solutions?
Stand up pouches serve diverse industrial sectors including chemicals, pharmaceuticals, food additives, vitamins, nutraceuticals, personal care products, detergents, and specialty powders. Any industry requiring product protection, shelf visibility, and cost efficiency finds stand up pouch solutions valuable for maintaining product integrity and meeting customer expectations.
How does a stand up pouch compare to traditional drum or bucket packaging for industrial chemicals?
Stand up pouches provide superior space efficiency, lower transportation costs, and easier handling compared to rigid drums while maintaining comparable barrier protection. For smaller volume requirements or specialty chemical applications, a stand up pouch offers flexibility and reduced environmental impact without sacrificing product protection or seal reliability that industrial chemical manufacturers require.
Can stand up pouches accommodate hazardous or corrosive chemical products?
Yes, heavy-duty stand up pouches engineered with aluminum foil, specialized polyester films, and reinforced construction can safely contain corrosive chemicals, oxidizing agents, and hazardous substances when properly specified. Material compatibility testing and regulatory compliance verification ensure that a stand up pouch meets all safety requirements for classified chemical products across industrial distribution networks.