 EN
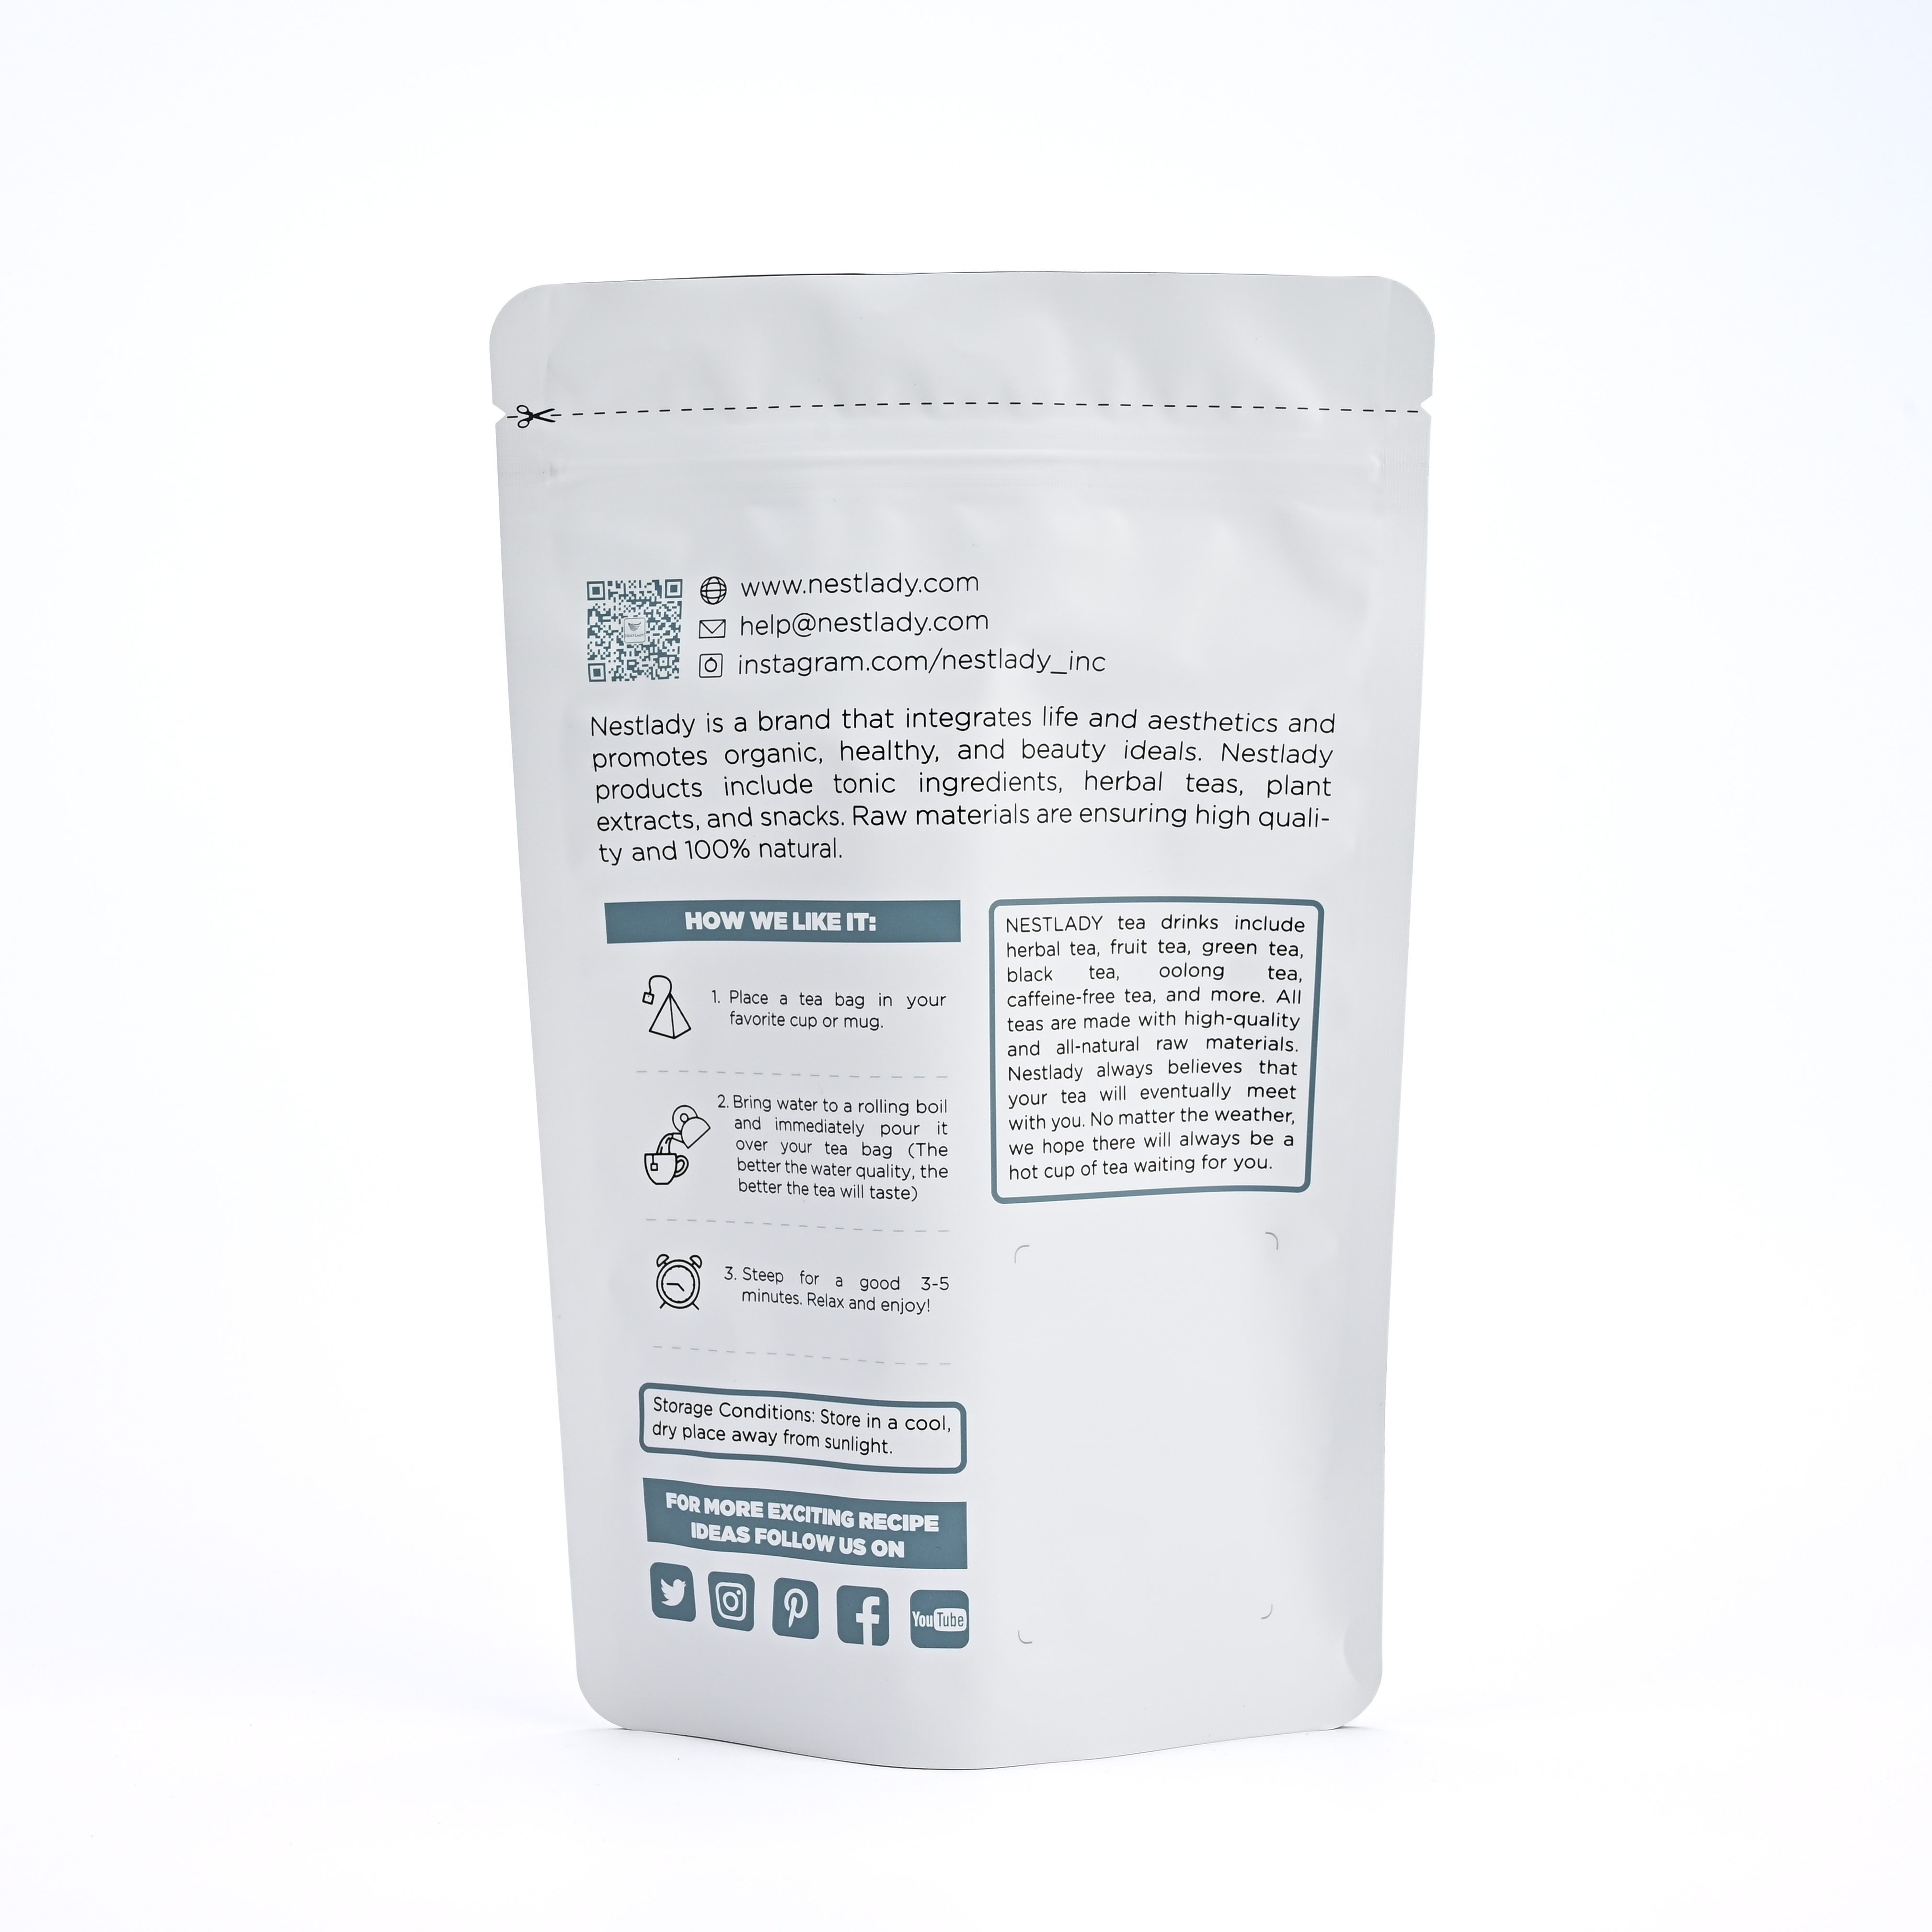
The success of flexible food packaging hinges on a component that often goes unnoticed by consumers yet determines whether products remain fresh, protected, and marketable throughout their shelf life. A zipper bag represents far more than a simple closure mechanism. It is the critical interface between product and environment, directly affecting moisture retention, contamination prevention, and consumer satisfaction. In industries ranging from snacks and spices to pet food and pharmaceuticals, the quality of the zipper bag can mean the difference between a product that thrives in the marketplace and one that fails to meet customer expectations.
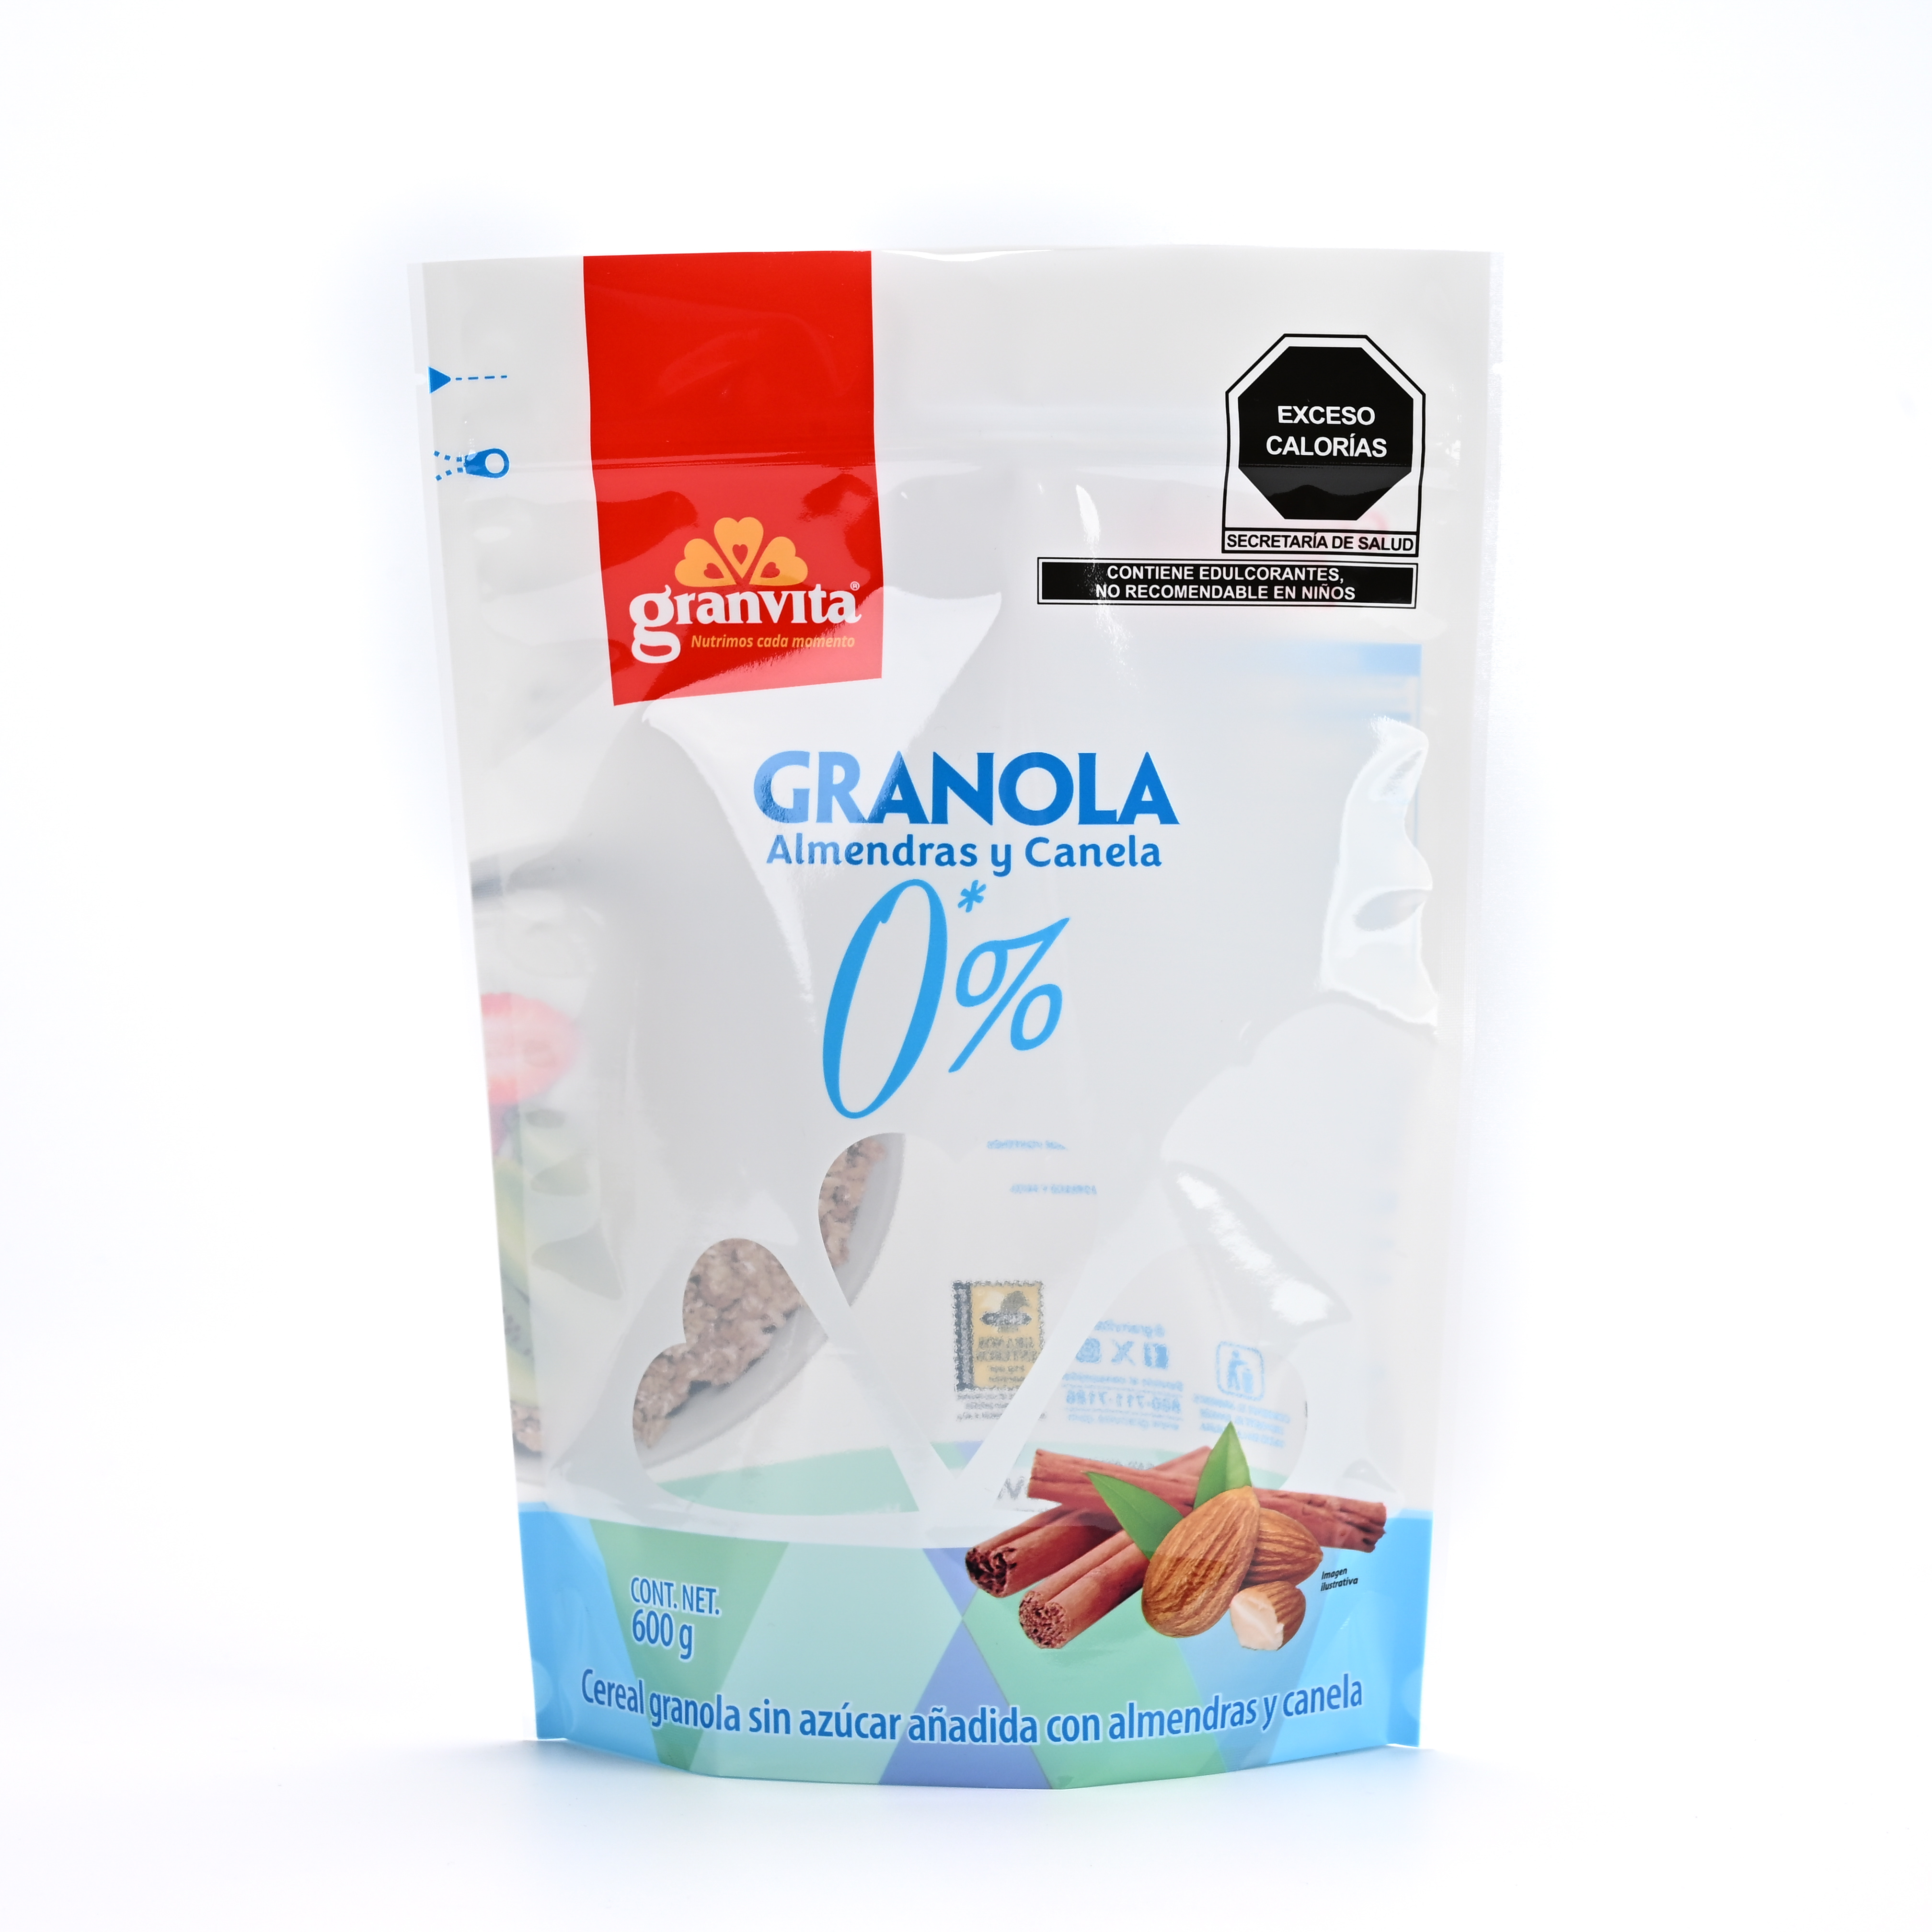
Flexible food packaging has revolutionized how manufacturers distribute and store goods, but this convenience depends entirely on the reliability of the zipper bag mechanism. When a zipper bag fails to seal properly, products lose potency, absorb unwanted moisture, or become exposed to oxygen that degrades quality. Premium zipper bag engineering ensures that every reseal operation maintains consistent barrier properties, protecting investments and brand reputation. Understanding why high-quality zipper bags matter provides manufacturers with the knowledge needed to make packaging decisions that enhance competitiveness and customer loyalty.
Why Premium Zipper Bag Design Matters for Product Integrity
Moisture and Oxygen Barrier Performance
The primary function of a zipper bag is to create a hermetic seal that prevents moisture ingress and oxygen penetration. Low-quality zipper bags often feature weak slider mechanisms or misaligned track geometry, creating microscopic gaps that compromise barrier integrity. A high-quality zipper bag incorporates precision-molded tracks, smooth slider operation, and consistent engagement depth that ensures every seal meets stringent barrier specifications. When moisture seeps into packaging containing dried herbs, coffee, or powdered supplements, product degradation accelerates exponentially. Premium zipper bag construction eliminates these failures by maintaining seal integrity across thousands of open-close cycles, a critical requirement for products expected to remain fresh for months.
Mechanical Durability and Consumer Experience
Consumers judge product quality by their interaction with packaging, and the zipper bag is the primary touchpoint. A smooth, responsive zipper bag creates confidence and satisfaction, while a stiff, difficult-to-operate slider frustrates users and damages brand perception. High-quality zipper bag mechanisms employ optimized slider weights, friction-balanced track surfaces, and reinforced attachment points that withstand repeated opening and closing without degradation. The zipper bag that fails prematurely—where the slider separates from tracks or becomes stuck—creates negative consumer experiences and liability risks. Manufacturers who invest in premium zipper bag quality report higher customer retention and reduced returns, making the investment economically justified beyond initial material costs.
Barrier Technology and Package Longevity in Food Applications
Multilayer Material Integration with Zipper Bags
Modern flexible food packaging combines multiple material layers—polyethylene, polypropylene, aluminum foil, and specialty films—to create comprehensive barrier systems. The zipper bag must integrate seamlessly with these multilayer substrates, maintaining structural integrity across the seal zone. High-quality zipper bag designs feature track profiles engineered to grip diverse film thicknesses and material combinations without slipping or misalignment. When a zipper bag is improperly designed for the substrate, stress concentrates at the seal interface during opening and closing, causing delamination or micro-tears that compromise the entire barrier system. Premium zipper bag engineering addresses these challenges through material compatibility testing and precision dimension control, ensuring the zipper bag performs reliably across the full range of flexible packaging configurations manufacturers employ.
Temperature and Environmental Stress Resistance
Food products experience thermal cycling during storage, transportation, and retail display. A zipper bag exposed to temperature fluctuations must maintain seal integrity as materials expand and contract. Low-quality zipper bags feature rigid plastic components that become brittle at cold temperatures or lose shape stability at elevated temperatures, causing seal failure. The superior zipper bag incorporates materials selected for elastic recovery, thermal stability, and resistance to stress-induced degradation. This performance becomes especially critical for frozen foods, where repeated freeze-thaw cycles stress the zipper bag mechanism. Manufacturers serving cold-chain applications specifically require premium zipper bag specifications because failures in frozen-food packaging create safety risks and substantial financial losses. The investment in high-quality zipper bag technology directly protects supply chain reliability and regulatory compliance.
Regulatory Compliance and Brand Protection Through Superior Zipper Bags
Food Safety Standards and Zipper Bag Certification
Food packaging must meet rigorous regulatory requirements established by agencies including the FDA and European Food Safety Authority. A zipper bag used in food applications must comply with material migration limits, seal-strength specifications, and contamination-prevention standards. Premium zipper bag manufacturers conduct independent testing and maintain certified compliance documentation, while budget alternatives often lack these assurances. When regulatory agencies investigate food contamination incidents or product recalls, the zipper bag design and manufacturing quality become central to liability determinations. Manufacturers who specify high-quality zipper bags with full compliance certification protect themselves against regulatory penalties and legal exposure. The zipper bag represents the last physical barrier protecting consumer health, making compliance-certified designs non-negotiable for responsible brands.
Market Differentiation and Consumer Trust
Premium brands recognize that product packaging communicates quality and reliability to consumers before purchase. A zipper bag that feels substantial, operates smoothly, and seals securely reinforces perceptions of premium quality. High-quality zipper bag design allows manufacturers to differentiate from competitors through tangible performance advantages that consumers experience directly. The zipper bag that fails or performs poorly generates negative reviews and reduces purchase intent for subsequent purchases. Brands competing in categories like premium coffee, specialty snacks, and natural supplements increasingly specify superior zipper bag technology as a market-positioning strategy. The zipper bag becomes a silent but powerful brand ambassador, communicating quality through user experience rather than advertising claims.
FAQ
What makes a zipper bag resist moisture and extend product shelf life?
High-quality zipper bags create reliable hermetic seals through precision-engineered track geometry and smooth slider mechanisms that maintain consistent contact pressure across the entire seal interface. Premium materials and manufacturing tolerances ensure the zipper bag resists micro-leakage from repeated opening and closing cycles. When barrier performance is optimized, the zipper bag prevents moisture vapor transmission and oxygen infiltration, keeping products fresh for extended periods and reducing waste-related losses for both manufacturers and consumers.
How do zipper bags withstand thermal stress during cold-chain storage?
Superior zipper bag designs incorporate thermally stable materials and elastically responsive components that maintain seal integrity through temperature cycling. Premium-grade polymers used in the zipper bag slider and track assembly resist embrittlement at freezing temperatures and maintain dimensional stability at elevated temperatures. Testing protocols for high-quality zipper bags specifically validate performance across the full range of temperatures the product will experience, ensuring the zipper bag protects food quality throughout cold-chain distribution and consumer storage.
Why should manufacturers invest in certified, compliant zipper bags?
Premium zipper bags manufactured under compliance-certified processes meet FDA and international food safety standards for material migration, structural integrity, and contamination prevention. When regulatory agencies investigate food safety incidents, the zipper bag documentation becomes central to liability determinations. High-quality zipper bags with certified compliance protect manufacturers from regulatory penalties, product recalls, and legal exposure. The zipper bag represents the critical barrier protecting consumer health, making compliance certification essential for responsible food packaging brands seeking to maintain regulatory standing and consumer trust.